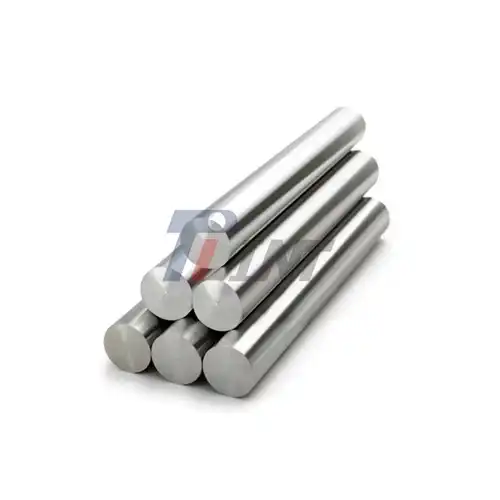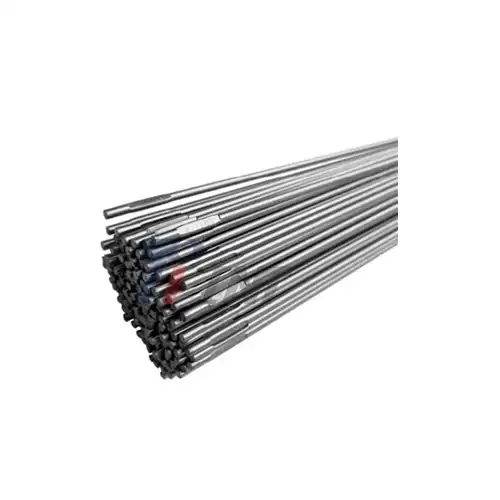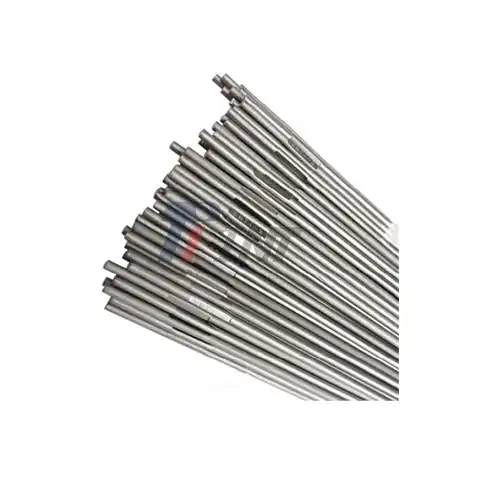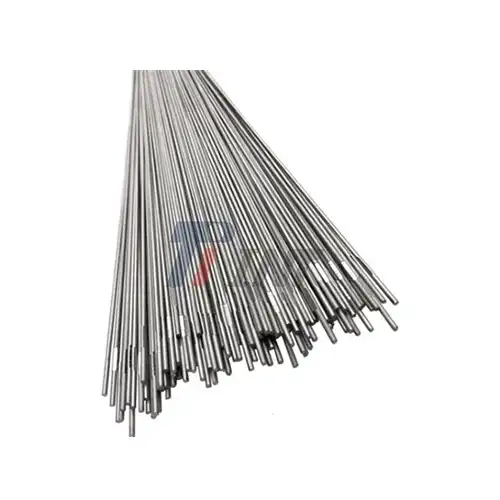
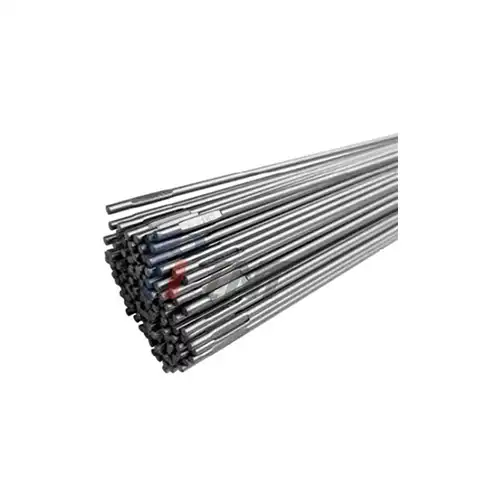
Gr2 Titanium Welding Wire


Corrosion-resistant for long-term use.
High strength-to-weight ratio for flexibility.
Excellent fatigue resistance for durability.
Customizable to suit needs.
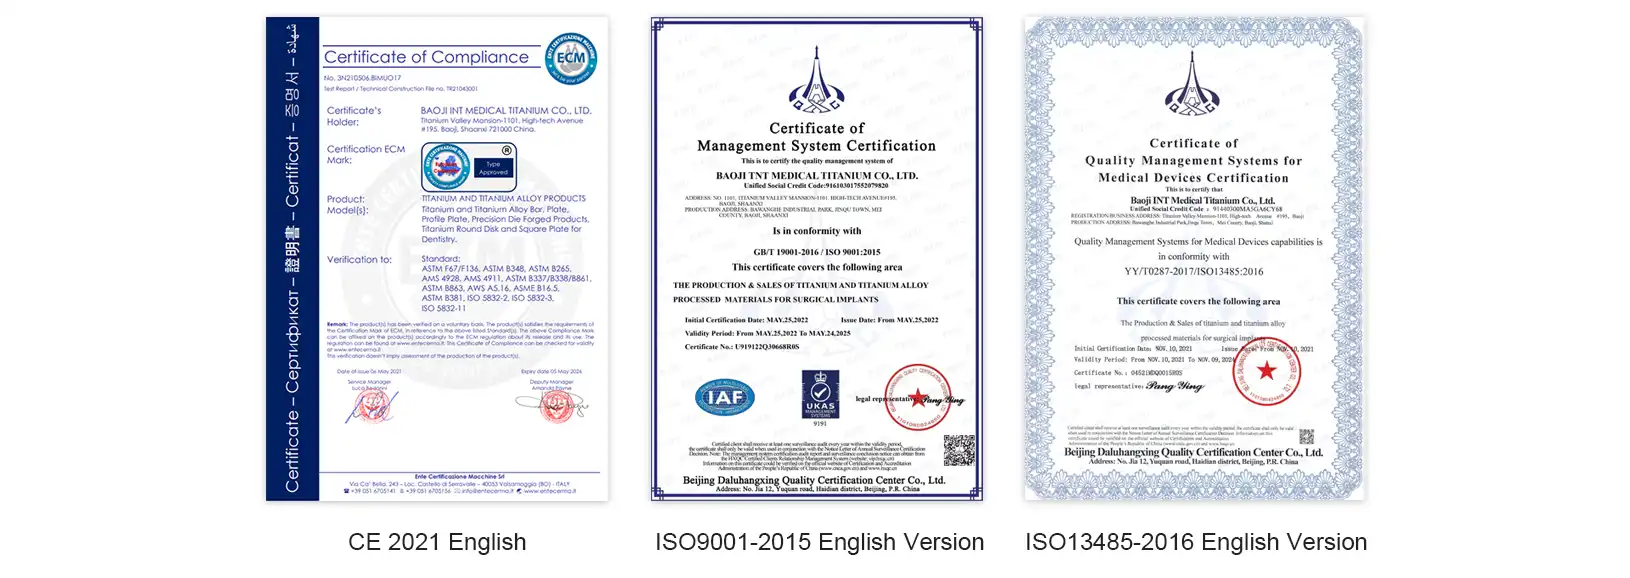
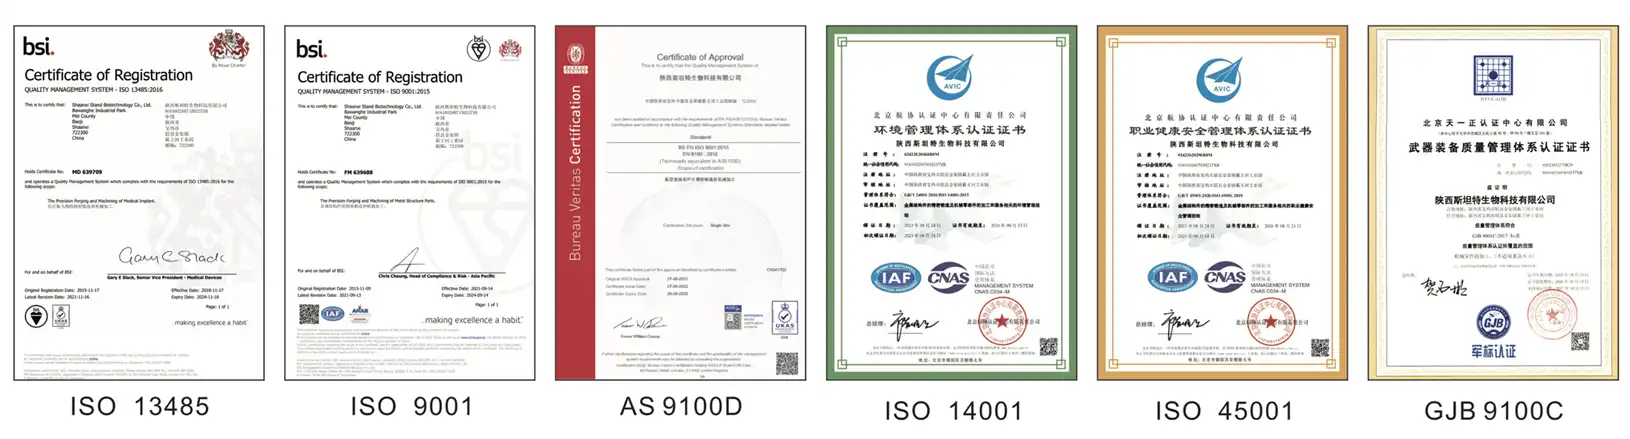
All products have passed ISO9001:2015, ISO13485:2016, EU CE safety certification
Gr2 Titanium Welding Wire: Premium Commercially Pure Titanium Filler Metal for Industrial Applications
Baoji INT Medical Titanium Co., Ltd., founded in 2003 with over 30 years of titanium industry expertise, manufactures Gr2 Titanium Welding Wire (ERTi-2 per AWS A5.16) engineered for demanding fusion welding operations. Our commercial grade titanium filler metal has tight interstitial control—Oxygen ≤0.25%, Hydrogen ≤0.015%, Iron ≤0.30%—to ensure consistent weld integrity across aerospace fabrication, chemical processing equipment and marine system installations. Our wire is ISO9001:2015, ISO13485:2016 and EU CE certified. Tensile strength is 345–450 MPa and elongation is >20%. Hermetic joints withstand chlorine, nitric acid and seawater corrosion where austenitic stainless steels fail.
What Makes Gr2 Titanium Welding Wire the Industry Standard?
This single-phase alpha microstructure filler metal is the workhorse for combining ASTM B265 Grade 2 base materials. It solves the most important fabrication problems by strict control of the composition, preventing hydrogen embrittlement of pressure vessels.
The wire has a density of 4.51 g/cm³, making it 45% lighter than steel equivalents. The melting temperature of 1660 °C and the spontaneous production of an oxide layer of TiO2 provide self-healing corrosion protection in both reducing and oxidising conditions.
The product maintains ductility in as-welded states, unlike Ti-6Al-4V alloys, which require sophisticated heat treatment. This removes the need for post weld processing expenditures and provides a yield strength of 275 MPa – enough to provide structural integrity without sacrificing formability.
Technical Specifications and Chemical Composition
|
Property |
Specification |
Standard |
|
Tensile Strength |
≥400 MPa (50–65 ksi) |
AWS A5.16 |
|
Yield Strength |
≥275 MPa (40 ksi) |
ASME SFA-5.16 |
|
Elongation |
≥20% |
ASTM B863 |
|
Density |
4.51 g/cm³ |
- |
|
Melting Point |
~1660°C |
- |
|
Oxygen Content |
≤0.25% |
AWS A5.16 |
|
Hydrogen Content |
≤0.015% |
ASTM B863 |
|
Iron Content |
≤0.30% |
AWS A5.16 |
|
Nitrogen Content |
≤0.03% |
- |

The chemistry ensures weld beads remain ductile rather than brittle. Oxygen levels stabilize the alpha phase while iron provides controlled solid-solution strengthening. Hydrogen caps prevent delayed cracking in high-stress applications.
Superior Corrosion Resistance for Aggressive Environments
Your fabrication jobs where normal alloys would corrode need materials that can survive chemical attacks. Our wire produces fusion zones resistant to pitting in moist chlorine, strong nitrates and marine atmospheres.
If scratched, the titanium dioxide protective film will rebuild itself. This self-healing property prevents catastrophic failures in heat exchangers and desalination systems that operate at high temperatures.
Tests show no weight loss after 10,000 hours of exposure to boiling 10% sulphuric acid. Compare this with 316L stainless steel in intergranular corrosion under the same conditions.
Critical Quality Control Procedures for Zero Defects
As per AWS A5.16 provisions, INT performs stringent inspection practices:
Surface Finish Verification: We do magnification testing to assure brilliant chemically pickled surfaces. Any residue of matte finish or drawing lubricant is immediately rejected to avoid weld porosity before shipment.
Interstitial Element Analysis: Inert Gas Fusion (IGF) instrument confirms Hydrogen below 150 ppm. This prevents delayed cracking in load bearing elements subjected to cyclic stress.
Positive Material Identification: XRF spectroscopy proves the material is pure titanium, removing incidental Ti-6Al-4V contamination that adds undesirable hardness in commercially pure applications.
All Weld Metal Tension Testing: Destructive testing of each production lot is conducted in accordance with ASME Section IX. Results are always over 345 MPa minimum standards with a homogeneous elongation distribution.
Application Solutions Across Multiple Industries
Chemical Processing Equipment: Use our Gr2 Titanium Welding Wire for fabricating reactors handling corrosive acids and alkalis. The wire maintains mechanical properties at temperatures up to 300°C while resisting stress corrosion cracking.
Marine and Offshore Systems: Seawater piping, condenser tubes, and hull components require fusion zones immune to chloride-induced failures. Our filler metal delivers 50-year service life in splash zones.
Aerospace Fabrication: Join commercially pure titanium airframe components where weight reduction directly improves fuel efficiency. The wire's high specific strength enables thinner gauge construction without compromising structural integrity.
Medical Device Manufacturing: Surgical instruments and implantable components benefit from biocompatible weld zones meeting ISO 13485 standards. Zero nickel content eliminates allergic reaction risks.
Proper Storage and Handling Guidelines
Titanium reactivity calls for thorough pre-weld pretreatment. Store wire spools in sealed containers with desiccant packs to keep <40% relative humidity.
Clean base metals with acetone or methanol before welding. Clean out all shop oils, drawing chemicals and oxide scale within 2" of the joint surfaces.
Argon shielding gas purity levels are maintained at 99.995%, with dew points below -50°C. The trailing shields protect the cooling weld beads until their surface temperature drops below 400°C, the level of air contamination.
Preheating is not required for most uses. However, when assemblies are above 6 mm thick they should be heated to 50-100°C to minimise temperature gradients and residual stress.
Why Choose INT as Your Trusted Supplier?
You can validate our titanium expertise, with 30+ years of experience, into a manufacturing consistency. Each spool is accompanied by mill test results certifying chemical, tensile characteristics and lot traceability.
We operate dedicated medical grade production lines that are free from cross contamination from industrial titanium streams. ISO 13485:2016 accreditation proves our devotion to our cleanroom and documentation control.
Custom spools for your automated welding systems. Typical choices include 0.8mm to 3.2mm diameters on 1kg, 5kg or bulk reels. Special packaging and cut lengths available on request.
Technical support experts develop welding procedure specifications (WPS) appropriate to your equipment and joint combinations. We provide support in the development of process qualification records (PQR) as dictated by code authorities.
Product Technology and Production Process
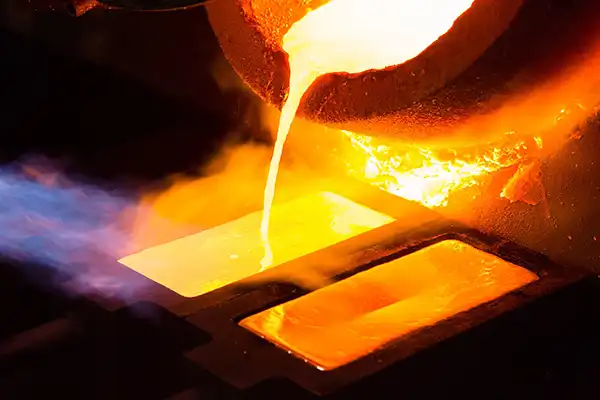
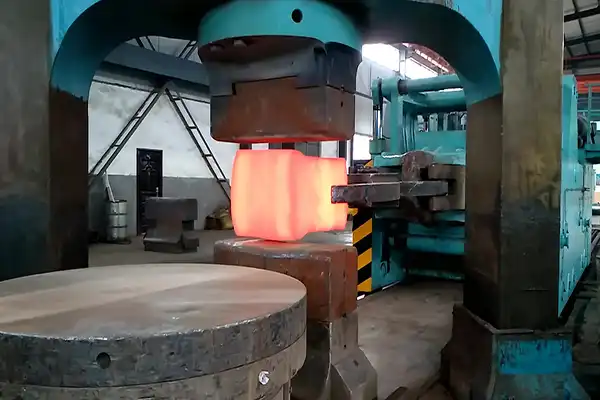
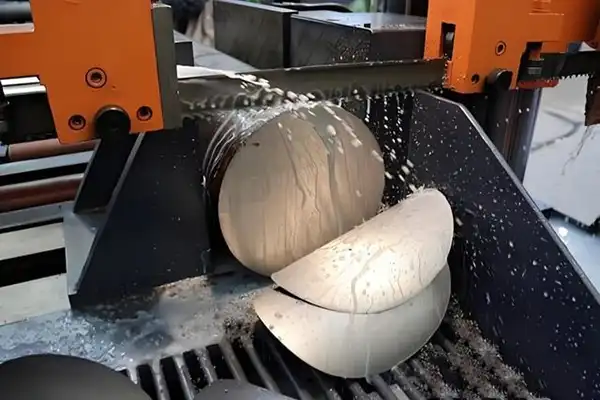
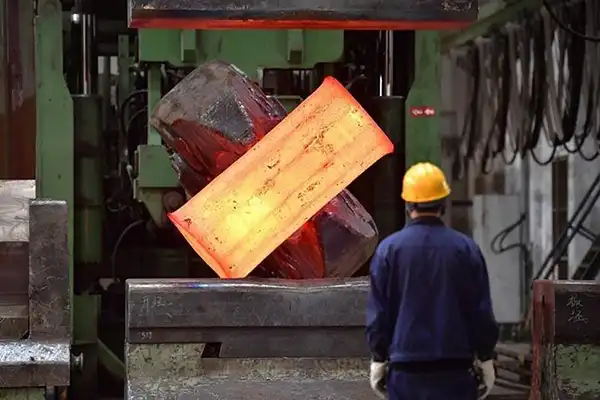
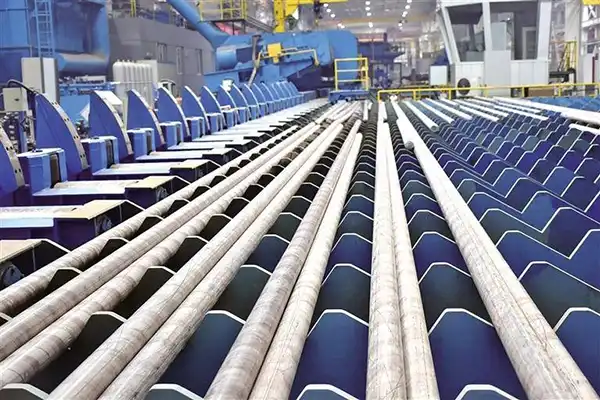
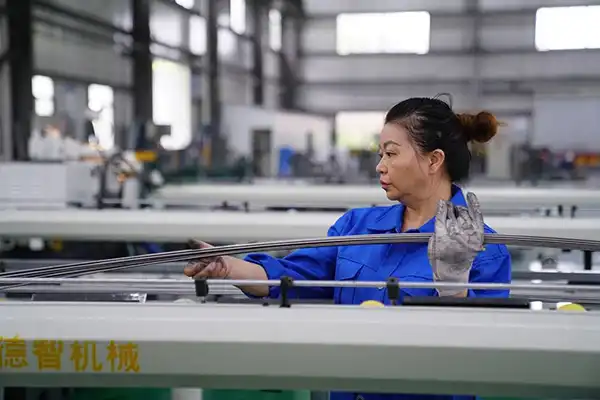
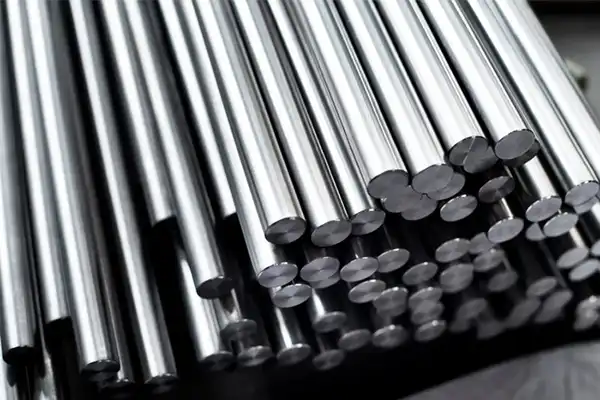
Hot rolling and forging techniques that enhance the mechanical properties, ensuring superior strength and toughness.Ultrasonic testing to detect flaws and ensure 100% reliability.
Strict quality control at every stage of production, meeting and exceeding international medical standards like ISO9001:2015 and ISO13485:2016.
 |
 |
 |
 |
 |
 |
 |
 |
Industries Catered
Our products are widely used in medical, automotive, aerospace, chemical, scientific and technological manufacturing and electronic information industries.
 |
 |
 |
 |
 |
 |
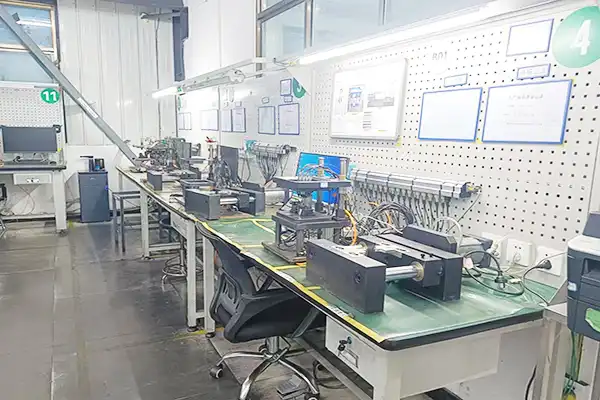
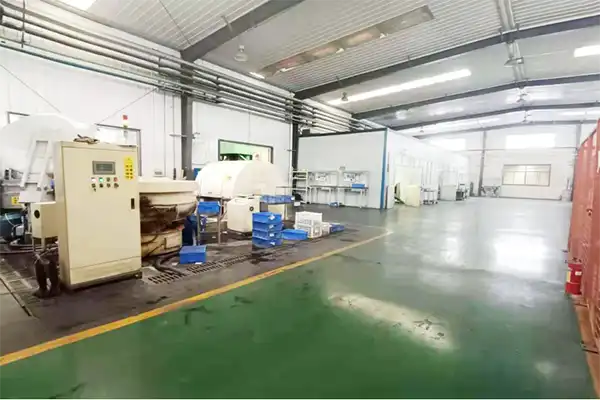
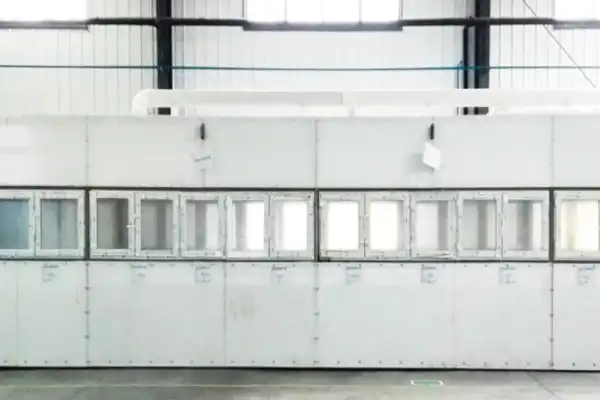
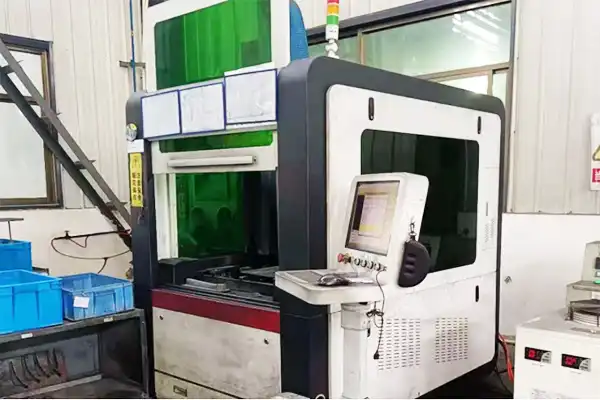
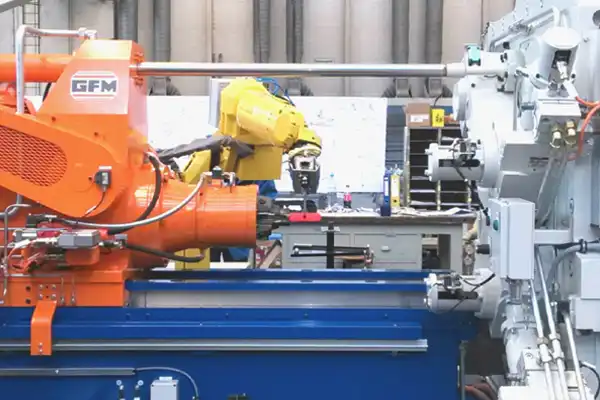
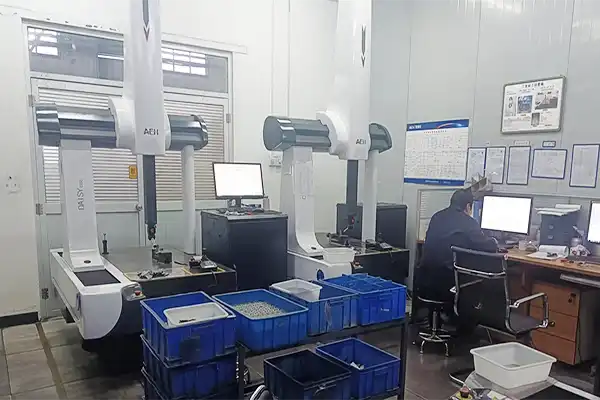
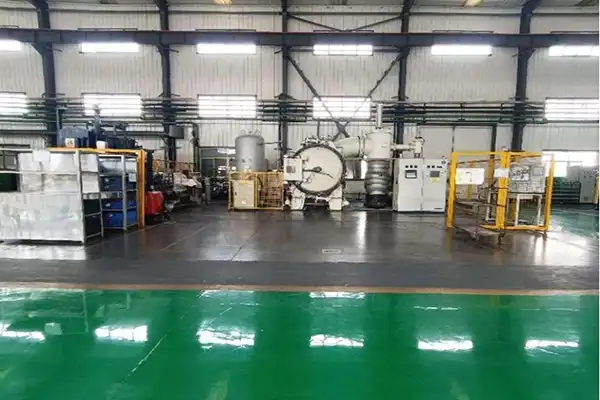
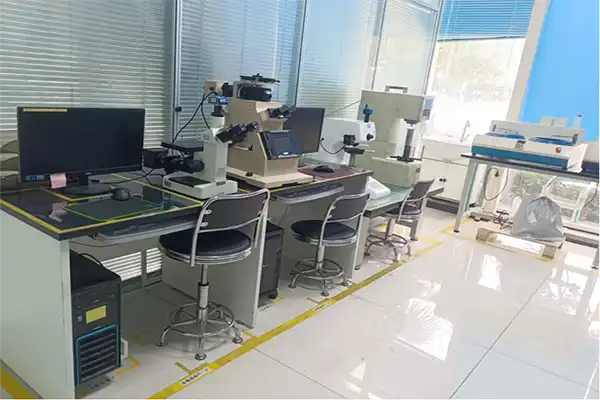
Our Factory - A Legacy of Excellence
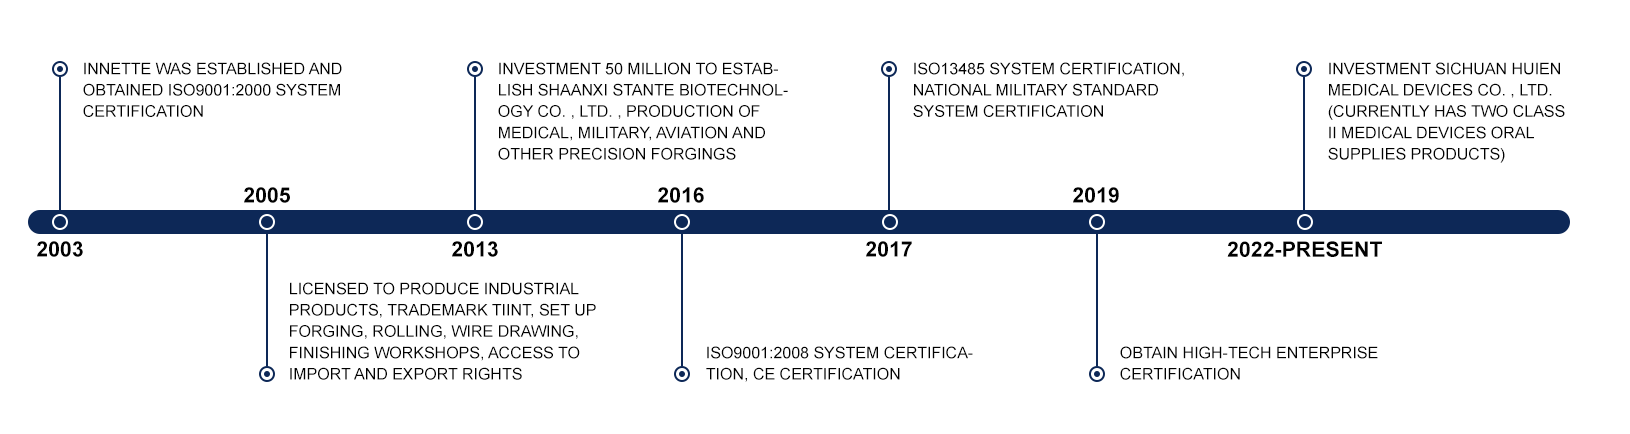
Founded in 2003 by titanium industry expert Mr. Zhan Wenge, Baoji INT Medical Titanium Co., Ltd. has grown into a benchmark enterprise in the R&D and production of medical titanium materials. With more than 30 years of experience, INT is deeply invested in the development of high-quality titanium for the medical sector. We provide a full range of titanium products, including pure titanium, Ti6Al4V ELI titanium, and custom titanium alloy forgings.
 |
 |
 |
 |
 |
 |
 |
 |
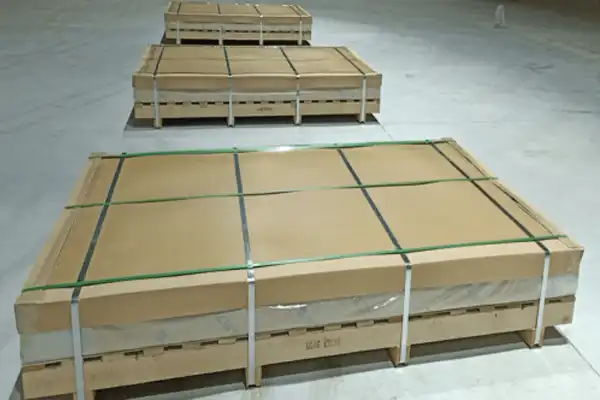
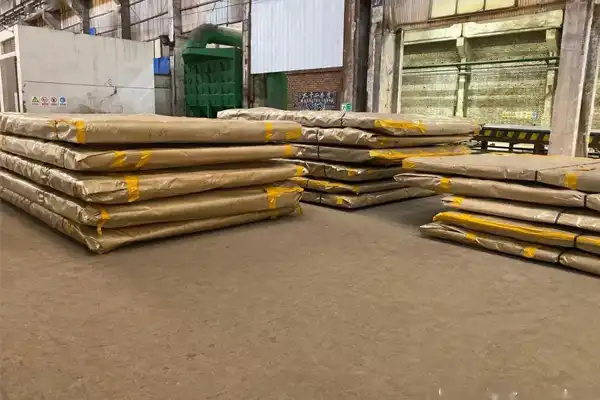
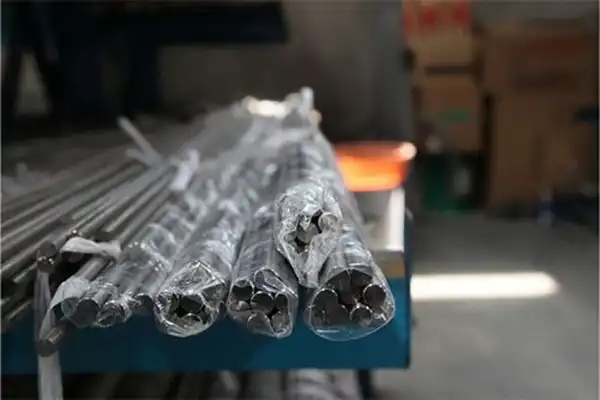
Packaging and Transportation
 |
 |
 |
Why Choose Us?
Choosing Baoji INT Medical Titanium Co., Ltd. means partnering with a trusted leader in the medical titanium industry.
Here’s why:
Proven Expertise: Over 30 years of experience in medical titanium production.
Advanced Technology: State-of-the-art production lines and equipment.
International Certifications: ISO9001:2015, ISO13485:2016, and EU CE certifications.
Comprehensive Support: We provide ongoing technical support, ensuring our products fit seamlessly into your manufacturing process.
Customer-Centric Approach: Committed to delivering high-quality products on time, every time.
For inquiries or orders, please contact us at export@tiint.com. We look forward to partnering with you for your medical titanium needs.
FAQ
Q: What welding processes work with the product?
A: The wire performs excellently in GTAW (TIG), plasma arc, and orbital tube welding applications. It feeds smoothly in automated MIG systems with proper drive roll configuration.
Q: How does Gr2 compare to Grade 5 titanium wire?
A: Grade 5 (Ti-6Al-4V) offers higher strength but requires post-weld heat treatment. Gr2 provides superior ductility and corrosion resistance in as-welded conditions—ideal when formability outweighs tensile requirements.
Q: Can this wire join dissimilar titanium grades?
A: Yes. Use it to weld Grade 2 to Grade 1 or Grade 7 base metals. Avoid joining to Grade 5 without consulting engineering, as thermal expansion mismatches may induce cracking.
Q: What causes porosity in titanium welds?
A: Inadequate gas shielding, contaminated wire surfaces, or excessive moisture introduce porosity. Our chemically pickled wire eliminates surface variables when paired with proper argon coverage.
Q: Do you offer ultra-low interstitial (ELI) versions?
A: Custom ELI specifications with hydrogen <80 ppm are available for cryogenic and high-cycle fatigue applications. Contact our technical team for minimum order quantities.
Contact Us for Technical Support and Quotations
Partner with INT for reliable Gr2 Titanium Welding Wire deliveries backed by comprehensive quality documentation. Request samples, certifications, or project-specific consultations by reaching export@tiint.com today.